When recycling scales reach 10,000 solar panels, traditional small-scale dismantling methods can no longer meet efficiency and environmental requirements. Instead, there is a need for a comprehensive industrialized technology system. This paper will discuss which technology can you use in the recycling process for 10,000 used solar panels.
What challenges does recycling 10,000 photovoltaic panels present?
The recycling of 10,000 photovoltaic panels faces multiple challenges arising from large-scale operations.


Which technologies are suitable for large-scale solar panel processing?
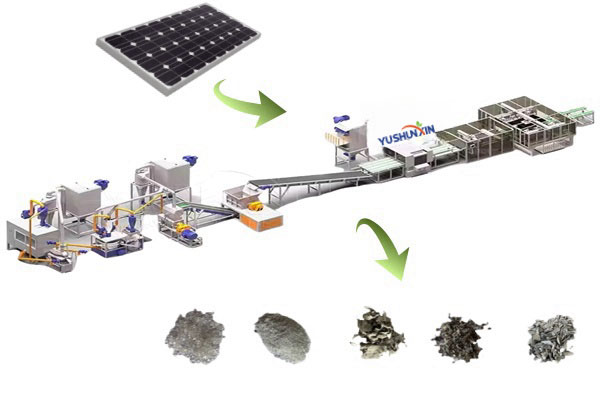
In the background of recycling large quantities of photovoltaic modules, photovoltaic panel recycling technology should focus primarily on mechanical separation, pyrolytic delamination, and chemical purification.

First, photovoltaic panels undergo mechanical disassembly by solar panel disassembly equipment, which gradually separates the aluminum frame, junction box, glass, and cell layers. Meanwhile, the intelligent recognition and sorting system can automatically identify the dimensions and structural type of photovoltaic panels and realize precise classification processing. The system’s processing capacity reaches 80 ku 100 modules per hour.

The robust adhesion of the EVA encapsulation layer within photovoltaic panels poses a critical challenge in separating the glass from the solar cells. PV pyrolysis technology employs a continuous pyrolysis system to decompose EVA under an oxygen-free environment at approximately 450–600°C. Consequently, this enables the complete separation of the glass substrate from the silicon layer.
After delamination, the solar cells can undergo a chemical wet process to remove surface impurities and residual adhesive.
Common acid and alkali solutions are controlled according to their ratios to achieve efficient desorption. At the same time, this control also minimizes emissions of harmful gases and waste liquids.
Chemical methods play a crucial role in achieving precise separation and surface purification throughout the entire process. Therefore, they provide assurance for safe and environmental disposal.

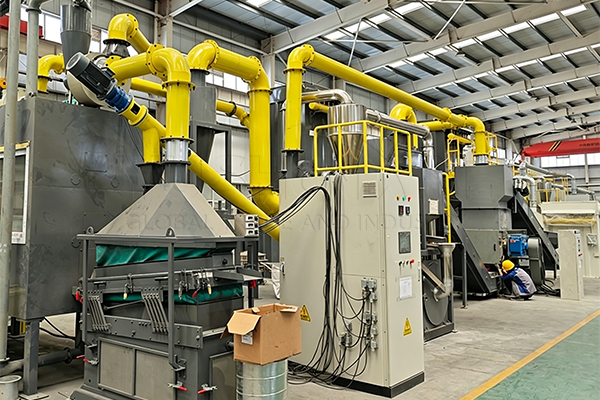
Recycling of waste liquid through neutralization reactors enables water resource reuse. While the waste gas goes through a cooling tower, activated carbon adsorption tower, and exhaust gas burner for purification and discharge in compliance with standards. Finally, vibrating screen separator and magnetic separation machine classify and recycle the solid residue.